01 · Thin-wall cover
Pump cover
Stepped, domed cover with a bolt circle. A flat parting and one closed cavity.
Drag to orbit, pinch or scroll to zoom.
The mould
Two bolted halves, 6 clamp bolts, 2 registration keys, 1 vent, a horizontal parting, so it stands on half A with the gate on top. Wall 6.2 mm on average, 6.0 mm at the thinnest.
Partingplane at z -0.18 mm
Ceramic389 cm³ vs 735 cm³ as a block
Half massesA 315 g, B 449 g
Gating and charge
One gate from the reservoir, sized for 109 medallions. The funnel prints as its own part on the FS-40 spigot.
Charge1,231 g
Yield40.9%
Gate bore26 mm
Funnel127.4 mm tall, 136.9 mm wide
Freezing check
The fast solidification check marks 1 spot to look at before the first pour. The map shows it.
- Spot 1 at (13, -29, 12) mm. 29,726 mm³ of metal, 1,784 mm³ of predicted shrink.
Last metal to freeze103 s
Build plate
2 moulds with funnel placed in one 305 mm build, minimum clearance, checked on the triangles. One 3MF, ready to send.
Packing18% of the build volume
Build height170 mm
Design for casting checks
- shrink allowancepass
- mould envelopepass
- depowder accesspass
- alloy windowpass
- min wallpass
- min cored holepass
- draftpass
- hot spotspass
Automation: nothing left to model
Two closed mould halves, no hand-finishing; 1 item(s) for an engineer to review (solidification).
Work for a designer 0
Nothing here.
For an engineer to review 1
- solidification review the hot spots: add a riser/chill or thin the wall there (variable wall), then re-run
Download
02 · Bracket / arm
Bored arm
Long arm with a 24 mm and a 16 mm bore. Six clamp bolts.
Drag to orbit, pinch or scroll to zoom.
The mould
Two bolted halves, 6 clamp bolts, 2 registration keys, a foot so it stands upright. Wall 6.3 mm on average, 6.0 mm at the thinnest.
Partingplane at z 1.88 mm
Ceramic387 cm³ vs 456 cm³ as a block
Half massesA 251 g, B 526 g
Gating and charge
One gate from the reservoir, sized for 56 medallions. The funnel prints as its own part on the FS-40 spigot.
Charge628 g
Yield54%
Gate bore26 mm
Funnel103.2 mm tall, 110.6 mm wide
Freezing check
The fast solidification check marks 3 spots to look at before the first pour. The map shows them.
- Spot 1 at (45, -13, 12) mm. 31,434 mm³ of metal, 1,886 mm³ of predicted shrink.
- Spot 2 at (-20, -2, 19) mm. 938 mm³ of metal, 56 mm³ of predicted shrink.
- Spot 3 at (115, 0, 16) mm. 517 mm³ of metal, 31 mm³ of predicted shrink.
Last metal to freeze82 s
Build plate
13 moulds placed in one 305 mm build, minimum clearance, checked on the triangles. One 3MF, ready to send.
Packing22% of the build volume
Build height275 mm
Design for casting checks
- shrink allowancepass
- mould envelopepass
- depowder accesspass
- alloy windowpass
- min wallpass
- min cored holepass
- draft4 to review
- hot spotspass
- Draft on moulded walls, 1 degree rule: 2 curved faces 24 mm tall: add 1 degree (0.419 mm of taper); 2 flat faces 24 mm tall: add 1 degree (0.419 mm of taper).
- Review note: 4 hole wall faces (24 and 16 mm holes) at 0 degrees. A printed core forms them or they are bored after casting, so they need no draft.
Automation: nearly there
Two closed halves; moldability left for a person to finish by hand; 1 review item(s).
Work for a designer 1
- moldability open 4.7 mm2 of cavity to the split or add a clean-out
For an engineer to review 1
- solidification review the hot spots: add a riser/chill or thin the wall there (variable wall), then re-run
Download
03 · Housing with cored passages
Cored manifold
Housing with internal passages that need printed cores.
Drag to orbit, pinch or scroll to zoom.
The mould
Two bolted halves, 4 clamp bolts, 2 registration keys, 1 vent, a foot so it stands upright. Wall 6.1 mm on average, 6.0 mm at the thinnest. 1 printed core, 1 seat cut.
Partingplane at z 100.48 mm
Ceramic569 cm³ vs 581 cm³ as a block
Half massesA 776 g, B 291 g
Gating and charge
One gate from the reservoir, sized for 154 medallions. The funnel prints as its own part on the FS-40 spigot.
Charge1,748 g
Yield53.5%
Gate bore26 mm
Funnel142.2 mm tall, 153.1 mm wide
Freezing check
No isolated pockets. The heaviest section freezes last, outside the feeder, so a riser or chill goes there. The map shows where.
Last metal to freeze229 s
Build plate
1 mould with funnel placed in one 305 mm build, minimum clearance, checked on the triangles. One 3MF, ready to send.
Packing15% of the build volume
Build height142 mm
Design for casting checks
- shrink allowancepass
- mould envelopepass
- depowder access6 to review
- alloy windowpass
- min wallpass
- min cored holepass
- draft4 to review
- hot spotspass
- 4 faces: depowder access.
- Draft on moulded walls, 1 degree rule: 4 flat faces 120 mm tall: add 1 degree (2.095 mm of taper).
- Review note: 8 hole wall faces (14 and 8 mm holes) at 0 degrees. A printed core forms them or they are bored after casting, so they need no draft.
Automation: nearly there
Two closed halves; moldability, split left for a person to finish by hand; 1 review item(s).
Work for a designer 3
- moldability resolve 1571.5 mm2 of undercut (core, extra split piece or redesign)
- moldability open 1223.2 mm2 of cavity to the split or add a clean-out
- split review the parting: the part's parting line is freeform, a planar split at z=100.48 was used
For an engineer to review 1
- solidification review the hot spots: add a riser/chill or thin the wall there (variable wall), then re-run
Download
More demos
All demos →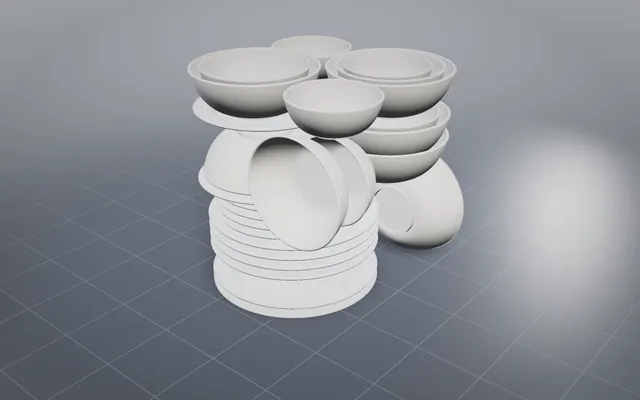
A whole dinner service nested in one SLS build
Bowls inside bowls and plates under plates, every gap proved on the real triangles before the build starts.
30 pieces, one SLS build GE bracket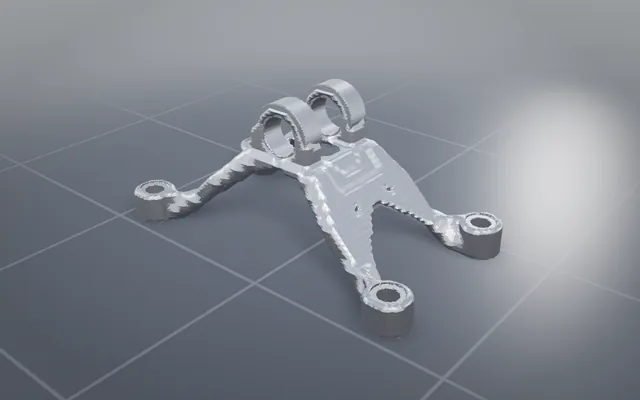
The GE jet engine bracket, lighter and carrying every load
The classic titanium bracket optimised and offered to print, cast, machine or weld, with STEP to download.
83.6% lighter Printed pendant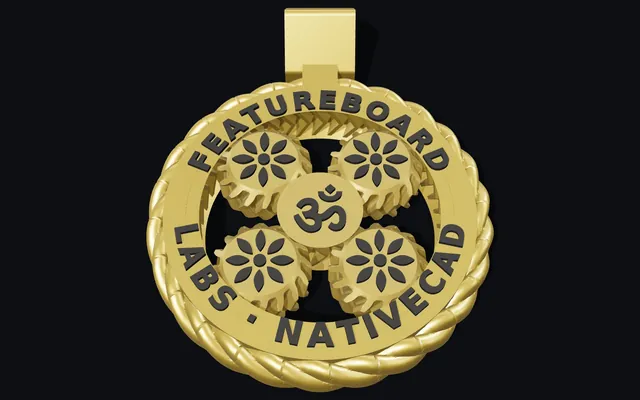
A planetary gearbox you can wear, printed in one piece
A working gearbox pendant that comes off a desktop printer already assembled and turning, in two colours.
5 moving parts, one print FEA loop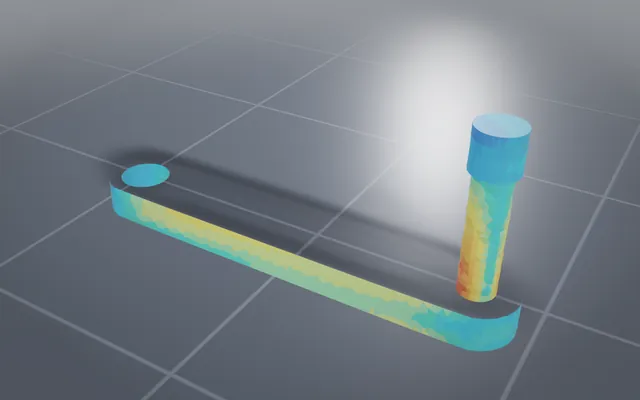
Finite-element analysis your agent can run
Stress and vibration results from the same AI session that built the part, with the peak and its margin.
6 designs solved in FEABuild your own part with NativeCAD
Try it free with the keyless evaluation · $200 per seat per year · Kernel SDK for products.